Table of contents
Assembly rarely makes headlines in quality assurance, yet it is where many product failures are born, and where the most cost-effective fixes still exist. Across electronics, automotive and medical devices, manufacturers face tighter tolerances, shorter lead times and rising scrutiny from regulators and customers, and that pressure is pushing quality teams to look beyond end-of-line testing. The overlooked truth is simple: if assembly drifts, every downstream inspection becomes a cleanup operation, not a guarantee of reliability.
Most defects are “made”, not “found”
How many failures are actually invisible at test? Quite a few, because functional testing is good at catching obvious non-conformance, but weaker at exposing latent defects that will only appear after thermal cycles, vibration, humidity or time. Industry data repeatedly points in the same direction: a large share of reliability problems trace back to assembly conditions such as solder joint integrity, component placement, contamination, torque control or handling damage. In electronics, for example, soldering-related issues remain a dominant root cause of field returns, and the reason is not mysterious, it is statistical; when you process thousands or millions of joints, even a tiny drift in paste volume, reflow profile or cleanliness multiplies quickly.
Quality assurance teams often inherit a bias toward inspection, partly because it is measurable and partly because it is easier to “add a test” than to redesign a process. Yet the economics are unforgiving. The classic cost-of-quality curve still holds: defects prevented upstream cost less than defects corrected downstream, and those corrected in the field are costliest of all, once logistics, warranty, brand damage and potential safety implications are counted. Studies from ASQ and other quality bodies have long highlighted how external failure costs can dwarf internal ones, especially when products are safety-adjacent. Assembly sits at the upstream choke point, where process capability determines how much risk will leak into shipping units, and where small investments in tooling, training and controls can reduce entire classes of defects rather than sorting them later.
Process control beats heroic inspection
Can you inspect quality into a product? Not sustainably, and experienced manufacturers know it. The more mature approach is to treat assembly as a controlled system, where the objective is not simply to produce units that pass today’s test, but to keep the process centered and predictable. That is the logic behind Statistical Process Control, capability indices and disciplined reaction plans, and it is also why modern factories increasingly instrument assembly steps. In electronics assembly, solder paste inspection, automated optical inspection and X-ray are often used, yet their real value rises when they feed back into the line in minutes, not when they generate a report after a shift ends.
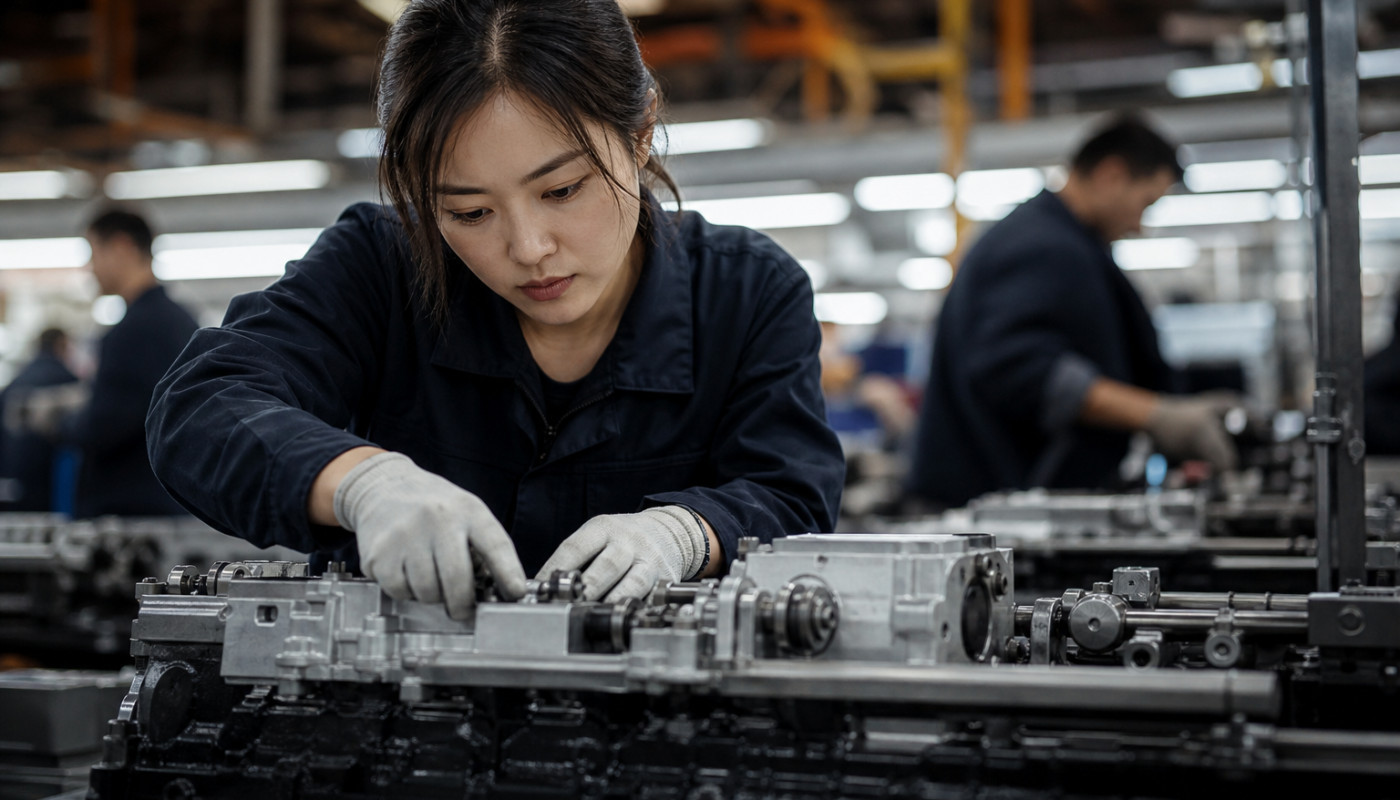
This is also where the deeper view of assembly matters, because it is not one step but a chain of interdependent operations. A change in incoming material lot, a nozzle wear issue on a placement machine, a minor shift in humidity, or a new operator on a manual station can all alter outcomes, and those outcomes may still “pass” until they suddenly do not. A precise description helps quality teams focus on what is controllable, and why documentation, traceability and training are not paperwork but risk management; Electronic manufacturing is an industrial process that consists of assembling different components onto a printed circuit board in order to perform a specific function. In practice, that function depends not only on design, but on repeatable execution, from component preparation and placement to soldering, inspection and final validation, with each interface offering opportunities for variation.
Assembly is where traceability becomes decisive
When a customer reports a failure, time is your enemy. The fastest route to containment and root cause is not guesswork, it is traceability that ties a shipped unit to the conditions under which it was assembled. That means lot and serial tracking for components, material certificates where relevant, and process data that can be queried quickly: reflow profiles, torque readings, press-fit forces, adhesive batch numbers, inspection images, operator IDs and timestamps. In regulated industries, such as medical devices, aerospace and automotive, that level of evidence increasingly separates suppliers who can respond in hours from those who spend days reconstructing what happened.
Traceability also changes behavior on the shop floor, because measurement has a disciplining effect. If an operator knows that a torque value is recorded and alarms will trigger outside limits, compliance improves, and variation shrinks. The same is true for ESD controls, cleanliness protocols and handling rules. Meanwhile, better traceability reduces the blast radius of a problem. Instead of broad recalls, a manufacturer can isolate a narrow window of suspect production tied to one material lot or one machine drift event. That precision is not only a cost issue, it is a credibility issue with customers and auditors, and it supports a more transparent relationship with insurers and certification bodies.
Design and assembly must talk earlier
Why do “hard-to-build” designs keep reaching production? Often because feedback arrives too late. Quality assurance becomes far more effective when assembly constraints inform decisions during design, prototype and pilot phases, not after volume ramps. Design for Assembly and Design for Manufacturability are sometimes treated as checklists, but their real power is cultural: they force engineering, manufacturing and quality to negotiate trade-offs early, when changes are still cheap. In electronics, that can mean revisiting pad geometries, component spacing, thermal reliefs and stencil strategies; in mechanical products, it can involve tolerance stack-ups, fastening access, poka-yoke features and simplified part counts.
The reward is measurable. Shorter ramp-up times, fewer engineering change orders after release, higher first-pass yield and more stable field performance tend to follow when assembly realities are embedded upstream. Even workforce factors matter. As experienced technicians retire in many industrial economies, manufacturers cannot rely on tacit knowledge to “make it work” at the line; they need assemblies that are robust to normal human variation, supported by clear work instructions, proper fixturing and error-proofing. That is how assembly becomes not the last step before shipping, but a central pillar of quality assurance, bridging what was designed on screen and what survives in the real world.
Plan, budget, and audit the line
Start with a line audit, then map defects and data gaps, and budget for the few controls that remove the most risk. Schedule a pilot run with enhanced traceability, and validate reaction plans under stress. Look for local or sectoral support programs for industrial modernization, then align them with training and metrology needs. Reserve time for supplier reviews, because assembly quality begins at incoming materials.
Similar
How Shared Work Environments Foster Creativity?
Incorporating Meeting Rooms In Flexible Work Environments

Navigating the future of workplace automation

Sustainable Business Practices The Competitive Advantage of Going Green in the Corporate World

How Detecting Website Themes Enhances Web Development And Design
